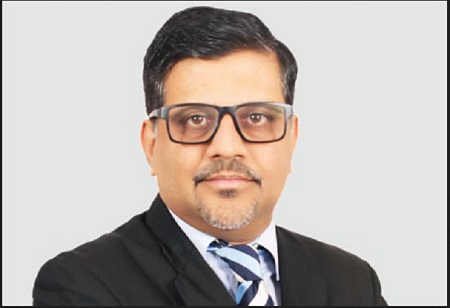
SAMS aims to compete with leading global equipment manufacturers while preserving the reliability, customization and value that have defined its journey
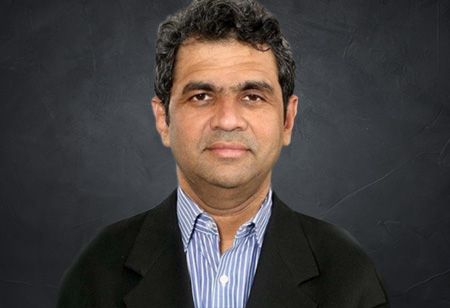
K. B. Bhandary, Chairman
Pharmaceutical process equipment manufacturing has undergone a fundamental shift over the past four decades. Where manufacturers once prioritized production capacity, mechanical durability and equipment longevity, the focus has expanded to process consistency, regulatory compliance, automation and seamless integration. Today, the challenge is not simply to manufacture a reliable machine, but to engineer a system capable of delivering repeatable outcomes with minimal operator dependency.
SAMS Engineering Solutions, backed by 45 years of industry experience, has evolved alongside these changing expectations. Beginning with pharmaceutical strip-packing machines, the company has expanded into customized processing equipment and integrated production lines. With more than 6,000 machines installed across 55 countries, SAMS has built its reputation on engineering reliability, customer relationships and an understanding of pharmaceutical manufacturing processes.
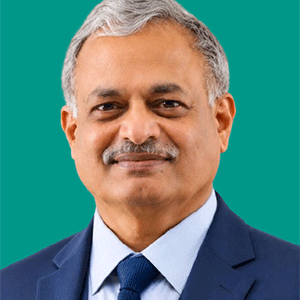
At the centre of this journey is K. B. Bhandary, Chairman, SAMS Technomech Pvt Ltd, whose founding philosophy continues to guide the organization. Rather than persuading customers to purchase equipment, he believed in developing machines that customers would actively seek out for their performance and dependability. Today, supported by a new generation of engineering and technology professionals, he is steering SAMS toward comprehensive process accountability and intelligent manufacturing solutions.
Engineering Around the Process, Not the Catalogue
For SAMS, equipment development begins with understanding the customer's formulation, production requirements and operational constraints rather than recommending machinery from a standard catalogue. This process-driven approach allows the company to customize solutions according to specific manufacturing challenges while maintaining quality and reliability.
Its portfolio has expanded from strip-packing machines to sifters, blenders, dryers, Rapid Mixer Granulators (RMGs) and advanced automated processing equipment. Even its established product lines continue to evolve, with innovations such as integrated laser-printing capabilities in strip-packing machines.
Durability remains central to the company's engineering philosophy. SAMS continues to encounter customers operating machines purchased more than two decades ago, reflecting the robustness of its equipment. With customer retention approaching 95 percent, its growth has historically been driven largely by referrals and longstanding relationships rather than aggressive sales strategies.
From Equipment Supply to Complete Process Accountability
As pharmaceutical production lines become increasingly interconnected, coordinating equipment from multiple suppliers introduces challenges in integration, troubleshooting and process consistency. Recognizing these limitations, SAMS has expanded beyond standalone machinery to offer complete granulation lines and integrated manufacturing solutions. SAMS aims to compete with leading global equipment manufacturers while preserving the reliability, customization and value that have defined its journey
This transition enables the company to assume greater responsibility for the overall manufacturing process, providing customers with a single point of accountability. Equipment specifications, operating parameters and integration requirements are addressed within a coordinated engineering framework rather than managed independently.K. B. Bhandary, Chairman
Supporting this evolution is SAMS's investment in in-house capabilities spanning process engineering, equipment design, automation and technical support. The company is also strengthening engineering documentation, structured validation and project-management practices to align with international manufacturing expectations.
Its growing team includes professionals with international training and experience in pharmaceutical applications, equipment design and process technology. Together, these capabilities are transforming SAMS from an equipment supplier into a comprehensive engineering partner.
Building Intelligence into Pharmaceutical Manufacturing
Automation and digital integration represent the next phase of SAMS's technological development. As pharmaceutical manufacturers face increasingly stringent expectations concerning data integrity, traceability and repeatable processing, intelligent equipment controls are becoming essential.
SAMS's APEx control platform supports this direction, alongside capabilities oriented toward 21 CFR Part 11 requirements and improved equipment connectivity. However, the company considers regulatory alignment a fundamental requirement rather than the ultimate objective of innovation.
Its technology roadmap encompasses Industrial Internet of Things (IIoT) connectivity, remote diagnostics, predictive maintenance and artificial intelligence and machine learning applications. The objective is to move beyond detecting process deviations toward systems capable of anticipating variations and supporting proactive corrective actions.
SAMS is also exploring Process Analytical Technology (PAT) and closed-loop control systems, particularly for oral solid dosage manufacturing, where powder characteristics and processing parameters directly influence product consistency.
The Road Ahead: Toward Autonomous Manufacturing
Looking ahead, SAMS is investing in research into continuous manufacturing and exploring highly automated production environments inspired by the dark-factory concept, where manufacturing processes operate with minimal manual intervention.
Beyond equipment innovation, the company plans to strengthen its global service network and establish application laboratory and process-support capabilities. These initiatives will help customers optimize formulations, adapt processes to equipment and address manufacturing challenges from early development through validation.
For Bhandary, the future of pharmaceutical engineering lies in moving beyond equipment transactions toward long-term responsibility for manufacturing outcomes. SAMS aims to compete with leading global equipment manufacturers while preserving the reliability, customization and value that have defined its journey.
As pharmaceutical manufacturing advances toward connected and intelligent production systems, SAMS intends to remain an engineering partner that not only supplies the machinery but also takes responsibility for the processes that make manufacturing successful.
, CDSCO.jpg "Fostering a Quality Culture in the Pharmaceutical Industry")